

What Challenges Affect the Recycling Of Recycled Alnico Magnets Materials?
Material Contamination Issues
Contamination is one of the most significant obstacles in Alnico magnet recycling. Adhesives, coatings, and dopants from various manufacturers create complex contamination scenarios, reducing recovery yields. High-quality magnets free from excessive glue, paint, or foreign materials are easier to recycle compared to their contaminated counterparts.
Magnets contaminated with adhesives, coatings, or alloys from different producers present distinct challenges. These contaminants may require additional pre-treatment steps such as chemical stripping or mechanical cleaning, increasing operational costs and reducing the yield of recoverable materials.
The presence of unidentified dopants further complicates recycling. Without knowing the exact composition of these additives, recyclers cannot optimize their separation processes, leading to lower-quality recovered materials that may not meet specifications for reuse in high-performance applications.
Technical Processing Hurdles
The technical complexity of Alnico magnet recycling poses significant barriers to efficient material recovery. Labor-intensive manual disassembly is often necessary to extract magnets from electronic devices or machinery, making the process time-consuming and costly, especially for small or complex products where magnets are deeply embedded.
Effective recycling requires specialized facilities capable of handling high-temperature melting and precise chemical separation. The process demands equipment that can oxidize aluminum and titanium from slag and burr, which is critical for reproducing raw materials for cast Alnico magnets. These specialized facilities require significant investment in equipment and expertise. Learn more about the challenges and investments required.
The separation of constituent metals presents additional challenges. Alnico magnets contain aluminum, nickel, cobalt, and iron, with cobalt being the most valuable yet challenging component to recover. The recycling process must separate these metals while maintaining their purity and value for future applications.
What Challenges Affect the Recycling Of Recycled Alnico Magnets Materials
Supply Chain and Logistical Barriers
The recycling industry for Alnico magnets faces significant logistical challenges due to the lack of mature collection systems. Unlike established recycling streams for materials like aluminum or paper, few dedicated collection points exist for products containing Alnico magnets, limiting the volume of recyclable material available to processors.
Unpredictable waste streams create operational difficulties for recycling facilities. The composition, volume, and availability of end-of-life products containing Alnico magnets vary significantly over time, making it difficult for recyclers to maintain steady operations and plan for consistent supply chains.
Collection systems also struggle with the diversity of magnet-containing products. Alnico magnets are found in everything from small electronic devices to large industrial equipment. This variety requires different handling and processing techniques, making standardized approaches challenging to implement effectively.
What is the Value of Recycled Alnico Materials?
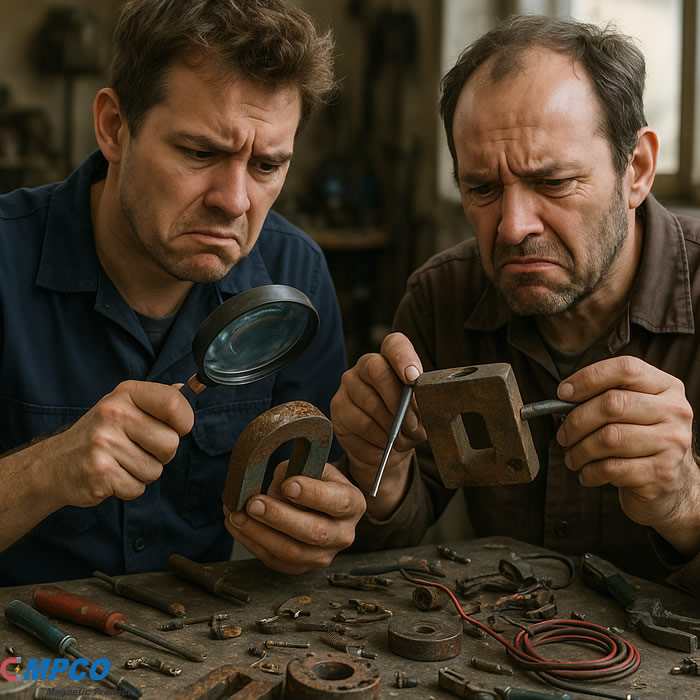
Technicians examining worn and corroded Alnico magnets with specialized tools on a cluttered workbench.
Recycled Alnico materials command significant market prices due to their high concentrations of valuable metals. Current scrap market prices range from $1.50 to $2.00 per pound for properly sorted and analyzed materials. This pricing reflects the substantial cobalt and nickel content that makes these magnets economically attractive for recovery operations.
The cost savings potential for manufacturing enterprises is substantial through standardized recycling programs. Companies implementing systematic Alnico recovery can reduce raw material procurement costs by 30% to 50% compared to purchasing virgin metals. These savings are particularly significant given the consistently high market prices for cobalt and nickel in recent years.
Cobalt is the primary value driver in Alnico recycling operations. This strategic metal is used extensively in battery production, aviation alloys, and high-temperature industrial processes. The purification and reuse characteristics of cobalt from Alnico sources make it highly suitable for secondary manufacturing applications. Nickel content adds additional economic value, enhancing the overall material worth during processing.
Environmental benefits create long-term economic value through sustainability compliance and resource conservation. Recycling Alnico materials reduces dependency on energy-intensive mining operations for cobalt and nickel extraction. This approach supports circular economy principles by keeping valuable materials in productive use rather than sending them to landfills. The environmental advantages align with corporate sustainability goals while generating measurable cost reductions in raw material sourcing.
Market conditions support strong valuations for recycled Alnico components. The strategic importance of cobalt in emerging technologies, combined with supply chain considerations, maintains consistent demand for recovered materials. Processing facilities can efficiently separate aluminum, nickel, cobalt, and iron components through established metallurgical techniques, preserving maximum value from each material stream.
Triangular Bar PTFE ALNICO V MAGNET
X Shape Magnet Stir Bar Alnico
AlNiCo5 Cylinder Cow Magnet with Curved Ends
Solid Alnico Blcok Bar Cow Magnet
AlNiCo3 Cylinder Rod Cow Magnet
AlNiCo 3 Cylindrical Rod Cow AlNiCo Rumen Magnet
Stainless Steel Round Edge Protect Cow Stomach Alnico Magnet
